In heavy manufacturing, the life expectancy of most equipment is often measured in years, not decades. Yet, some industrial conveyors prove that with the right design, materials, and maintenance, systems can reliably operate for nearly half a century.
One such example is a PRAB Conveyor, installed in the late 1970s at a U.S.-based manufacturer of refractory materials. After 48 years of continuous duty in one of the toughest environments imaginable, this conveyor has finally retired — setting an industry benchmark for durability and ROI.
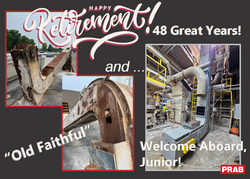
This facility produces advanced ceramic and metal oxide products for the aerospace and high-performance manufacturing industries. In the late 1970s, the plant required a conveyor that could withstand the rigors of handling dense, abrasive materials with high silica and zirconium content under high-temperature conditions.
The solution was a custom-engineered Roller Bucket Conveyor designed to resist abrasion, minimize wear, and keep operating under extreme stress.
Well-maintained by the facility’s staff — with only occasional support from PRAB — the conveyor performed with remarkable reliability across nearly five decades.
Over its operational life, “Old Faithful” endured:
This record underscores the true ROI of investing in heavy-duty industrial conveyors.
When the time came to replace the original unit, the facility didn’t open bidding to other suppliers. They went straight back to PRAB.
Why?
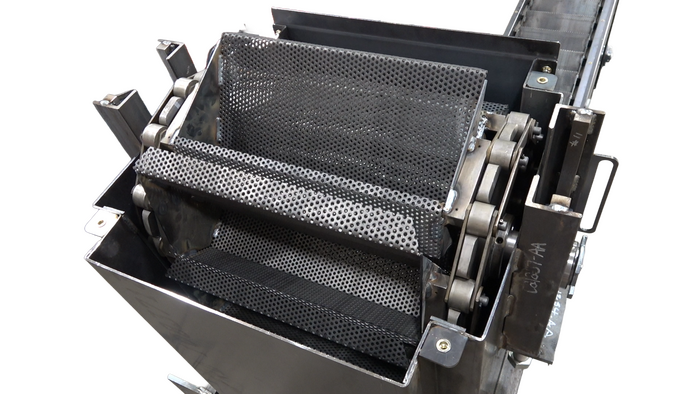
Today’s PRAB Roller Bucket Conveyor builds on the core durability of the original while adding modern improvements:
For manufacturers, equipment downtime can cost thousands of dollars per minute in lost productivity. That makes durability not just an engineering goal — but a financial strategy.
Long-life conveyors like the Roller Bucket system demonstrate how upfront investment in robust equipment translates into decades of savings, reduced maintenance, and operational continuity.
PRAB offers a complete line of metal scrap conveyors engineered for the most demanding industrial applications, including:
Each system is designed for longevity, serviceability, and integration with chip processing, fluid recycling, and scrap load-out systems.
This 48-year success story highlights three enduring lessons for manufacturers:
A conveyor that has served for nearly half a century becomes more than a piece of equipment — it becomes part of a plant’s legacy. With the right design, materials, and support, industrial conveyor systems can deliver value for generations to come.

 (800) 968-7722
 (800) 493-3462